United States | EN
 Canada | EN
 United Kingdom | EN
 German | DE
 France | FR
 Mexico | ES
 Japan | JA
 China | ZH
How to Section, Mount, Grind, Polish, Etch, and Analyze Titanium Samples for Metallographic Evaluation
Utilized for their high strength-to-weight ratio, biocompatibility, and corrosion resistance titanium and its alloys are suited to many demanding applications. For these applications, it is important to validate sample properties and performance. Through Titanium metallography, the analysis of features is possible following metallurgical preparation. Metallographic preparation consists of five steps: sectioning, mounting, grinding, polishing, etching, and analysis. Not all steps are required but each has benefits depending on processing priorities (sample quality, efficiency, throughput, etc.). Titanium presents unique challenges; its tendency to deform mechanically, smear during polishing, react to heat during cutting, and develop twinning artifacts makes preparation particularly demanding.
What Makes Titanium Difficult to Prepare Metallographically?
How Do You Section Titanium Samples Without Damaging the Microstructure?
Why Is Sectioning of Titanium Samples Necessary?
Sectioning is done to remove features of interest from the bulk material while minimizing thermal and mechanical damage. Some examples of features of interest are an implant cross-section for porosity evaluation, a weld zone, and a coating interface. Once the region of interest has been identified, sectioning can begin.
How To Decide on Abrasive Cutting or Precision Cutting
What Is the Difference Between Abrasive and Precision Blades?
Abrasive blades consist entirely of abrasive particles held together by a resin bond and gradually wear away during use. Titanium-specific abrasive blades use a relatively soft bond combined with silicon carbide abrasives to continually expose fresh cutting particles. Precision wafering blades use a metal substrate with abrasive bonded only to the outer rim. Buehler’s titanium-designated blades have diamond as their abrasive on the outer edge. To keep abrasive fresh and clear of waste material, dressing is done to wafering blades before cutting and even during cutting sometimes.
How Do I Section Titanium to Minimize Damage?
For precision cutting, Buehler recommends 15HC wafering blades, high RPM (4000-5000 rpm) and moderate feed rates (6-10 mm/min). For abrasive cutting, soft-bonded silicon carbide wheels used with pulse cutting provide effective performance while minimizing cutting damage. Titanium samples must be securely clamped to prevent movement during cutting. Any movement can create curved cuts, blade damage, or excessive mechanical deformation. If a sample shifts under modest hand pressure, fixturing should be adjusted before cutting begins. Maintaining low temperatures during sectioning reduces thermal damage, improves surface finish, and limits deformation. To do this, all titanium sectioning should be performed with abundant coolant directed into the cut and blade. This will minimize the material removal required to reveal the true microstructure in later preparation steps.
How Do You Mount Titanium Samples for Metallography?
Is Mounting Required for Titanium Samples?
Mounting is not always required, but it frequently improves preparation quality and laboratory efficiency. Mounted titanium specimens can be easier to handle during grinding and polishing, especially when samples are small, irregularly shaped, or porous. Mounting also improves edge retention, supports automation, and increases throughput through sample uniformity. For failure analysis, additive manufacturing evaluations, and porosity assessments, mounting provides structural preservation of critical features.
What Mounting Method Is Best for Titanium Samples?
Sample sensitivity and site priorities help determine the best mounting method for an application. Hot compression mounting combines heat and pressure to encapsulate the sample. This method is good for routine titanium alloy samples that are not sensitive to elevated temperatures or pressures. Epoxy mounting is especially useful for structurally weak or mechanically sensitive specimens. Epoxies have low shrinkage, great edge retention, and high adhesion, with low curing temperatures but with long curing times (1-9 hours). They are able to fill gaps and support weak features during grinding. Contrary to epoxies, acrylic systems have shorter cure times between 5 and 30 minutes. However, while they lead in speed, they lack sample adhesion and exhibit higher viscosity than epoxy. They still suit instances where speed is the priority. If both efficiency and mount quality are important, a UV acrylic system could work. Though properties of UV-activated acrylics are better than traditional acrylics, their shrinkage performance does not surpass that of epoxy.
How to Grind and Polish Titanium?
Why Is Grinding and Polishing Needed?
The goal of grinding and polishing is to produce a surface that is flat, scratch-free, and reveals the true microstructure. Grinding removes the damage from sectioning and produces a flat surface; polishing removes finer levels of deformation to yield a scratch-free surface. If these artifacts are not removed, they can be mistaken for features, leading to inaccurate conclusions during analysis. Preparation must minimize common issues such as relief, pullout, pitting, smearing, edge rounding, and embedded abrasive particles. Surface quality affects the ability to perform analysis. Because of this, metallographers often consider grinding and polishing to be the most important stages in the entire preparation process.
What Is a Grinding and Polishing Method for Titanium?
| Table 7.1: 3-Step Method for Ti Alloys | |||||
|---|---|---|---|---|---|
| Sectioning | Abrasive Cutter with a wheel recommended for use on ductile materials | ||||
| Mounting | Compression, typically with EpoMet | ||||
| Surface | Abrasive / Size | Load - lbs [N] / Specimen | Base Speed | Relative Rotation | Time [min:sec] |
| CarbiMet | 320[P400] grit Sic water cooled | 6[27] | 300 |
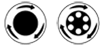
|
Untile Plane |
| UltraPad | 9μm MetaDi Supreme Diamond* | 6[27] | 150 |
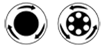
|
10:00 |
| ChemoMet | 0.02-0.06μm MasterMet Colloidal Silica** | 5[22] | 150 |
|
10:00 |
Image -  - Specimen Holder -  *Plus MetaDi Fluid Extender as desired **Attack polish may be used, 1 part Ammonium Persulfate solutions (10g Ammonium Persulfate per 100ml distilled water) or 30% Hydrogen Peroxide to 5 parts Silica |
|||||
| Image & Analysis | Grain Size, Measurement & Analysis Applications | ||||
| Hardness Testing | Vickers | ||||
What Are Common Issues Encountered When Polishing Titanium?
With slow material removal rates, operators can be tempted to increase grinding pressure or preparation times. However, excessive pressure can introduce surface defects and artifacts. Artifacts can remain visible even after polishing and may be mistaken for actual microstructural features. Care must be taken to use appropriate loads (5lbs for a 1.25” sample), maintain adequate lubrication (the polishing surface must be well damped throughout the step), and avoid unnecessarily aggressive preparation conditions.
How Do You Etch Titanium to Reveal Its Microstructure?
Is Etching Required for Titanium Analysis?
After polishing, titanium specimens are typically etched to reveal features such as grain boundaries, phase distributions, and processing characteristics. Polished surfaces can sometimes reveal structures but often look featureless under Bright Field light. Cross-polarized light can be used to examine structure in the unetched condition, and can be used to confirm the quality of the polish.
What Etchant Should I Use for Titanium?
Depending on the composition and processing of the titanium sample, the effectiveness of solutions can change. Finding the correct solution could take multiple attempts and preparation cycles. The most common etchant is Kroll’s Reagent: 100 mL water, 1-3 mL hydrofluoric acid and 2-6 mL nitric acid.
Often, etching times can be a few seconds when swabbing, up to several seconds during immersion. There are two methods for traditional etching: swabbing and immersion. Swabbing uses an item like a cotton ball with some etchant in it to gently expose the sample surface to the etchant. Immersion, as the name suggests, immerses the sample surface in etchant. Once complete, the etchant must be removed from the sample surface to stop the reaction or the surface can become over-etched. With swabbing, there is more control of area and intensity of exposure. Immersion allows for better consistency and larger areas to be etched at once. Kroll’s reagent is widely used for commercially pure titanium and alpha and alpha-beta titanium alloys. Modified Weck’s tint etchant can also be used when grain structure visualization is important. For even more potential etchants, take a look at the SumMet Guide etching section. Many titanium etchants contain hydrofluoric acid (HF), nitric acid, and strong oxidizers. Appropriate PPE, ventilation, chemical handling procedures, and waste management practices are essential.
What Kind of Analysis Can Be Done on Titanium?
Microstructural analysis, hardness testing, SEM, EBSD, porosity measurement, and failure analysis can all be done on properly prepared sample surfaces. Because of its susceptibility to mechanical deformation and sensitivity to heat, good preparation practices are essential for revealing its true properties. With good practices, laboratories can consistently produce artifact-free surfaces.
For additional preparation methods, consumable recommendations, and application-specific guidance, link readers to Buehler’s Solutions by Material: Titanium and Titanium Alloys resource page and relevant titanium preparation technical notes.
Grinding and Polishing FAQs
Not all steps are required but each has benefits depending on processing priorities (sample quality, efficiency, throughput, etc.).
Titanium is both abrasion-resistant and highly sensitive to preparation-induced deformation. Improper preparation can introduce artifacts that alter microstructure, leading to inaccurate analysis.
Sectioning is done to remove features of interest from the bulk material while minimizing thermal and mechanical damage.
For precision cutting, Buehler recommends 15HC wafering blades, high RPM (4000-5000 rpm) and moderate feed rates (6-10 mm/min).
For abrasive cutting, soft-bonded silicon carbide wheels used with pulse cutting provide effective performance while minimizing cutting damage.
An attack-polishing additive is often mixed with the colloidal silica suspension to help remove the final traces of mechanical deformation and improve the quality of the polished surface before etching. In applications needing a higher level of surface quality, such as EBSD, color etching, or publication-quality imaging, a final vibratory polishing step may also be used to eliminate the last traces of deformation.
After polishing, titanium specimens are typically etched to reveal features such as grain boundaries, phase distributions, and processing characteristics. Polished surfaces can sometimes reveal structures but often look featureless. Cross-polarized light can show microstructure without etching and is often used to confirm polishing quality.
Kroll's reagent is widely used for commercially pure titanium and alpha and alpha-beta titanium alloys. Kroll's Reagent: 100 mL water, 1-3 mL hydrofluoric acid and 2-6 mL nitric acid. Modified Weck's tint etchant can also be used when grain structure visualization is important. For even more potential etchants, take a look at the SumMet Guide etching section.
Microstructural analysis, hardness testing, SEM, EBSD, porosity measurement, and failure analysis can all be done on properly prepared sample surfaces.
On This Page
- > How to Section, Mount, Grind, Polish, Etch, and Analyze Titanium
- > What Makes Titanium Difficult to Prepare
- > How do you Section Titanium Samples without Damage
- > How do you Mount Titanium Samples
- > How do you Grind and Polish Titanium
- > How do you Etch Titanium to Reveal its Microstructure
- > What Kind of Analysis Can Be Done on Titanium
- > Titanium Metallography FAQs
Need Help with your Sample Preparation?
Our application specialists can help you develop the right grinding and polishing process for your material and analysis needs.